
Pharmaceutical/Health
ATI provides clean room equipment with electro-mechanical operation, non-marking wheels, and stainless steel, zero-chip construction. Wheels are attached separately so that they are in pristine condition when they touch the floor. ATI knows precisely how to accommodate the special needs of the pharmaceutical and healthcare environments.
Specific Pharmaceutical/Health projects have included:
Pharmaceutical & Health Industry Cranes for Material Handling Solutions
The pharmaceutical and healthcare industries operate in highly regulated environments where safety, cleanliness, precision, and compliance are essential. From pharmaceutical manufacturing facilities and biotechnology laboratories to medical device production plants, hospitals, research centers, and distribution warehouses, organizations require reliable material handling systems that support efficient operations while maintaining strict quality standards.
Moving sensitive equipment, pharmaceutical ingredients, reactors, mixing vessels, cleanroom components, sterile processing systems, packaging materials, and finished products requires specialized lifting equipment designed to minimize contamination risks, improve worker safety, and enhance operational efficiency. In many pharmaceutical and cleanroom environments, stainless steel material handling equipment is preferred because of its corrosion resistance, easy sanitization, and compatibility with strict hygiene standards.
Air Technical Industries (ATI) has been designing and manufacturing material handling solutions since 1964. ATI provides both standard and custom-engineered lifting equipment that helps pharmaceutical manufacturers, biotechnology companies, healthcare facilities, and medical device producers improve productivity, reduce manual handling risks, and maintain regulatory compliance. ATI manufactures more than 2,500 standard and custom material handling products, including cranes, lift tables, upenders, manipulators, and positioning systems. Many of these solutions can be configured to support cleanroom and sanitary applications.
Why Material Handling Is Critical in Pharmaceutical Manufacturing
Modern pharmaceutical production facilities handle valuable equipment and materials throughout multiple stages of operation, including:
- Raw material receiving and storage
- Ingredient preparation and mixing
- Biopharmaceutical processing
- Tablet and capsule production
- Pharmaceutical packaging and labeling
- Sterile manufacturing
- Medical device assembly
- Laboratory testing and research
- Distribution and logistics operations
Many facilities continue to face challenges associated with manual lifting, repetitive motion injuries, equipment accessibility, contamination prevention, and limited workspace. Implementing properly designed cranes for pharmaceutical industry applications, including stainless steel lifting systems, helps address these challenges while improving safety, efficiency, and product quality.
Ergonomic lifting systems also support GMP requirements by promoting consistent handling procedures and reducing the likelihood of product damage, contamination risks, or operational errors.
Common Pharmaceutical Material Handling Challenges
Maintaining Cleanroom Standards
Cleanrooms require equipment and materials to be moved safely without introducing contaminants. Stainless steel cranes, lift tables, and positioning equipment are commonly used in these environments because they are easier to clean, resist corrosion, and help support stringent sanitation protocols.
Supporting GMP Compliance
Good Manufacturing Practices require controlled and repeatable processes. Proper lifting equipment helps standardize material handling activities while reducing risks associated with manual operations and contamination concerns.
Handling Heavy and Sensitive Equipment
Pharmaceutical facilities frequently move reactors, mixers, filtration systems, sterilization equipment, pumps, and processing vessels that can be difficult to handle safely without dedicated lifting solutions. Stainless steel equipment is often preferred when these operations occur in hygienic processing environments.
Improving Worker Safety
Manual lifting remains one of the leading causes of workplace injuries. Ergonomic cranes, lift-assist devices, and lift tables help reduce physical strain while improving workplace safety and productivity.
Maximizing Limited Floor Space
Many pharmaceutical facilities operate in tightly controlled environments where floor space is limited. Customized lifting solutions can improve workflow efficiency without disrupting production activities.
Pharmaceutical Industry Crane Applications
Cleanroom Equipment Handling
Cleanroom environments require precise movement of sensitive equipment while maintaining cleanliness standards. Stainless steel lifting equipment can safely position reactors, vessels, filtration units, processing equipment, and cleanroom components while minimizing contamination risks and operator contact.
ATI designs customized lifting equipment to meet unique cleanroom handling requirements and solve complex material handling challenges within confined production spaces.
Reactor and Mixing Vessel Maintenance
Routine maintenance often requires the removal and replacement of motors, pumps, gearboxes, agitators, and mixing assemblies. Mobile floor cranes and portable lifting systems provide maintenance teams with safe and flexible lifting capabilities while minimizing downtime.
Material Transfer Operations
Raw pharmaceutical ingredients are frequently delivered in drums, totes, bins, and bulk storage containers. Material handling equipment helps move these materials efficiently between receiving areas, storage locations, and production lines while supporting sanitary handling procedures.
Pharmaceutical Packaging Systems
Packaging operations require frequent equipment adjustments, component replacements, and maintenance activities. Cranes and lift tables allow operators to safely position equipment while improving productivity and reducing ergonomic risks.
Medical Device Manufacturing
Medical device production often involves handling precision components that require accurate positioning during assembly, inspection, and testing processes. Ergonomic lifting systems help improve quality control while reducing repetitive motion injuries. Stainless steel equipment is often used when cleanliness and corrosion resistance are critical.
Biotechnology and Laboratory Applications
Biotechnology facilities and research laboratories frequently require lifting solutions for process equipment, testing systems, laboratory vessels, and specialized production components. ATI’s custom-engineered equipment supports these highly specialized applications, including applications requiring stainless steel construction.
Health Industry Cranes for Hospitals and Healthcare Facilities
The healthcare industry faces unique material handling challenges beyond pharmaceutical manufacturing. Hospitals, laboratories, healthcare equipment manufacturers, and research facilities frequently require specialized lifting solutions for:
- MRI and imaging equipment installation
- Laboratory equipment positioning
- Sterilization system maintenance
- Medical equipment assembly
- Facility maintenance operations
- Storage and inventory management
- Equipment transportation and relocation
Health industry cranes provide controlled lifting capabilities that help protect sensitive medical equipment while improving workplace safety. For sterile and hygienic environments, stainless steel lifting systems can provide additional durability and sanitation benefits.
ATI Products for Pharmaceutical and Healthcare Applications
Reversible Boom Cranes
ATI’s Reversible Boom Cranes provide exceptional reach and flexibility for pharmaceutical maintenance, equipment installation, and production support operations. Stainless steel configurations can be provided for select cleanroom and sanitary applications.
Best Applications:
- Reactor maintenance
- Equipment installation
- Cleanroom equipment handling
- Laboratory operations
- Production line support
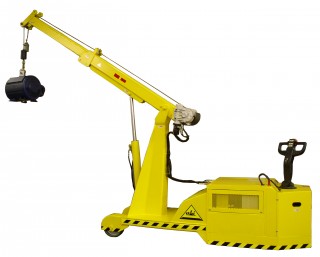
Super-Master Mobile Floor Cranes
When overhead crane systems are unavailable or impractical, mobile floor cranes provide portable lifting power for a wide range of applications.
Best Applications:
- Equipment changeovers
- Pharmaceutical maintenance departments
- Medical device manufacturing
- Warehouse operations
- Facility support functions
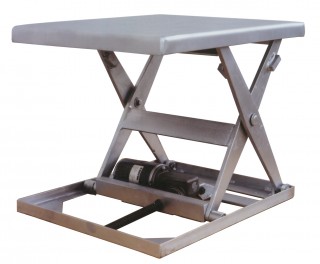
Zero-Low Lift Tables
Zero-Low Lift Tables improve workstation ergonomics while reducing worker fatigue and repetitive motion injuries.
Best Applications:
- Packaging operations
- Assembly processes
- Material staging
- Laboratory support
- Workstation optimization
Lift & Tilt Tables
Lift and Tilt Tables position containers, bins, and production materials at optimal working heights and angles for improved accessibility.
Best Applications:
- Ingredient handling
- Packaging operations
- Component assembly
- Bulk material processing
- Warehouse applications
Upenders
Upenders safely rotate containers, molds, equipment, and production components for improved handling efficiency.
Best Applications:
- Container inversion
- Equipment repositioning
- Production changeovers
- Medical device manufacturing
- Material processing operations
Benefits of ATI Pharmaceutical Material Handling Solutions
Enhanced Workplace Safety
Reducing manual lifting lowers the risk of musculoskeletal injuries, strains, and workplace accidents.
Improved Regulatory Compliance
Proper lifting equipment supports GMP initiatives by improving consistency, traceability, operational control, and sanitary material handling procedures.
Increased Productivity
Ergonomic lifting systems reduce cycle times, improve workflow efficiency, and allow personnel to focus on higher-value activities.
Reduced Product and Equipment Damage
Controlled lifting and positioning help protect sensitive pharmaceutical products, medical devices, and production equipment.
Stainless Steel Solutions for Hygienic Environments
ATI can provide stainless steel material handling equipment for applications where corrosion resistance, washdown capability, cleanability, and contamination prevention are critical requirements.
Custom-Engineered Solutions
ATI’s in-house engineering team develops application-specific lifting systems designed to meet specialized operational requirements, including cleanroom-compatible and stainless steel equipment solutions.
Request a Quote
Whether you need pharmaceutical industry cranes, health industry cranes, ergonomic lift tables, mobile floor cranes, cleanroom lifting equipment, stainless steel lifting equipment, biotechnology material handling systems, or a fully customized lifting solution, ATI can help optimize your operation with equipment designed for safety, precision, cleanliness, and regulatory compliance.
Our engineering team works directly with pharmaceutical manufacturers, biotechnology companies, laboratories, medical device producers, healthcare facilities, and distribution centers to develop lifting solutions tailored to specific operational requirements.
Request Your Quote Today to discover how ATI’s pharmaceutical material handling solutions can help streamline operations, improve workplace safety, support GMP objectives, maintain cleanroom standards, and increase productivity throughout your facility.
Frequently Asked Questions (FAQ’s)
1. Why are cranes used in pharmaceutical manufacturing?
Cranes improve workplace safety, reduce manual handling risks, support GMP compliance, increase productivity, and help protect valuable equipment and products.
2. Why is stainless steel equipment important in pharmaceutical facilities?
Stainless steel equipment is corrosion-resistant, easy to sanitize, durable, and well-suited for cleanroom and hygienic environments where contamination control is a priority.
3. Can cranes be used in cleanroom environments?
Yes. Custom-engineered lifting systems, including stainless steel cranes and material handling equipment, can be designed to meet cleanroom requirements and minimize contamination risks while supporting efficient equipment handling.
4. What types of material handling equipment are commonly used in pharmaceutical facilities?
Common equipment includes floor cranes, jib cranes, lift tables, upenders, manipulators, positioners, stainless steel lifting equipment, and custom material handling systems.
5. How do ergonomic lifting systems improve pharmaceutical operations?
Ergonomic systems reduce worker fatigue, improve accessibility, lower injury risks, increase productivity, and support consistent manufacturing processes.
6. Can ATI provide customized pharmaceutical lifting solutions?
Yes. ATI specializes in designing and manufacturing custom material handling equipment tailored to specific pharmaceutical, biotechnology, healthcare, medical device, and cleanroom applications, including stainless steel solutions.
.